
Wire EDM
Wire EDM, otherwise known as wire erosion, is commonly used to produce extrusion dies. It cuts using the same mechanism as die-sinking. However, the die is replaced with a very fine electrically charged wire which will work as the electrode. This machining method is comparable to a cheese cutter, making a two-dimensional cut in a three-dimensional part.
Description
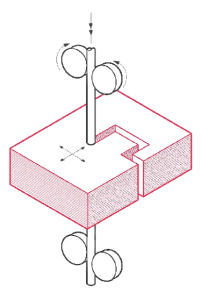
The wire is usually very thin, with a diameter of around 0.05mm to 0.35mm. A fresh wire is automatically spooled throughout the machining process to avoid using burnt wire and to ensure precise cutting. The below image illustrates the way wire is utilised in wire EDM:
This process will produce incredibly precise cuts. However, if you are looking to cut sharp inside corners, it’s important to note that wire EDM alone won’t be able to give you true square corners. The wire and spark gap will create a tiny radius of about 0.13mm to 0.15mm, but this can be smaller or larger depending on the diameter of the wire.
If that is not sufficient for your project, a small dog-bone corner can be applied to create perfectly square internal corners. Read our guide on how to machine square corners for more information on the best ways to machine sharp internal corners.
Sometimes it is necessary to start a cut from the centre of a part rather than from one of the edges. For example, machining a complex shape in the centre of an extrusion die. If that’s the case, hole drilling EDM can make a small hole for the wire to be threaded through for wire EDM machining.
Reviews
There are no reviews yet.